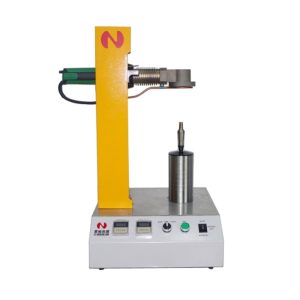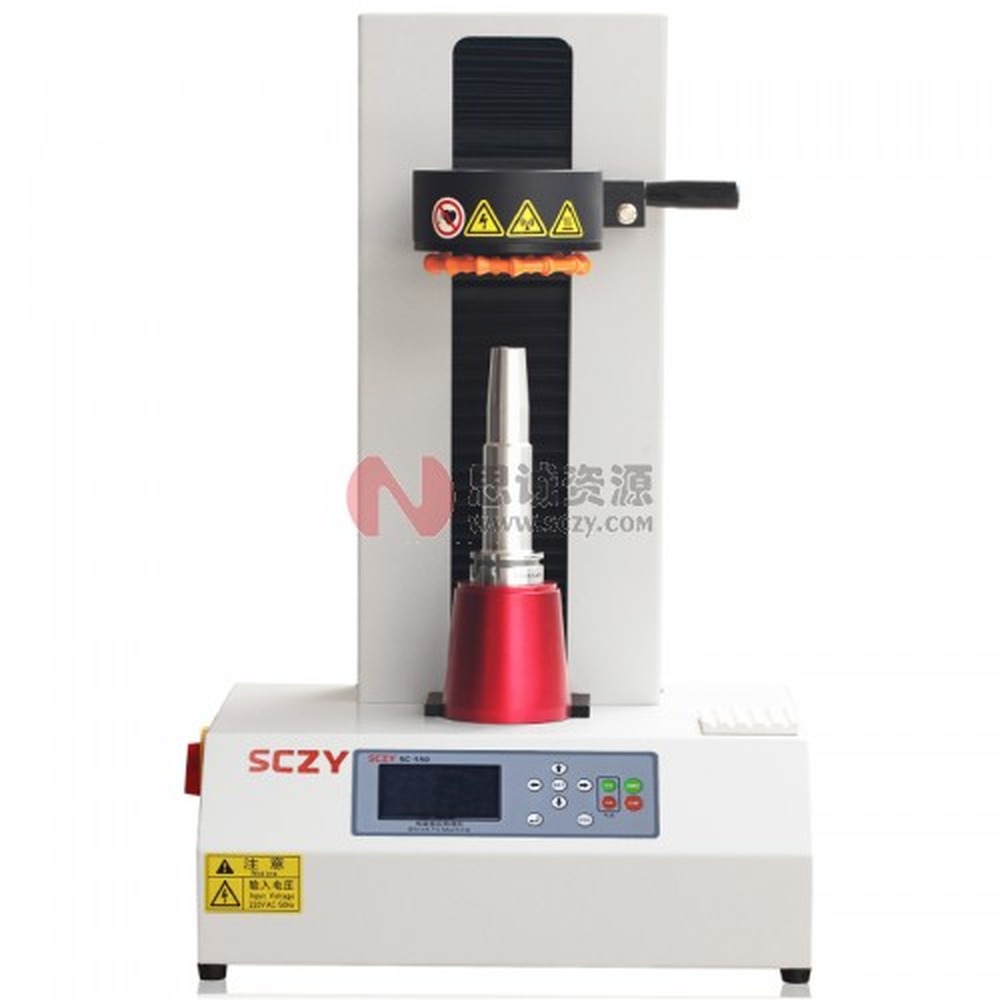
Electromagnetic induction heater.
Features
- The induction coil generates a high-frequency magnetic field that induces eddy current in the tool shank. Heat builds quickly, which shortens tool change time.
- Forced air cooling brings the shank back to room temperature fast.
- Once the shank reaches temperature, press the air start button to begin cooling. The shank stays where it is, which keeps the operation safe.
Heating Time Reference
Times below are for reference only. Actual results depend on the holder, the material and the operating conditions.
Cautions
- Never lift or move the heating head (induction coil) before the heating cycle finishes. Doing so will burn out the coil or the main board.
- Avoid overheating the shank — do not let it heat to red.
- Anyone with a heart stent or metal implants must stay clear while heating is in progress. Please read the manual carefully; we accept no responsibility for equipment failure or personal injury caused by improper operation.
- Keep the surface of the induction coil clean and dry.
| Wall Thickness / Size | Alloy Steel / sec | Stainless Steel / sec |
|---|---|---|
| 1.5T (bore 4-12 mm) | 3 | – |
| 3.0T (bore 4-8 mm) | 4-5 | 7-9 |
| 3.0T (bore 10 mm) | 5-6 | 7-9 |
| 4.0T (bore 12 mm) | 6-8 | 7-9 |
| 6.5T (bore 4-8 mm) | 10-12 | – |
| 6.5T (bore 10-12 mm) | 11-13 | – |
| 6.5T (bore 14-25 mm) | 11-15 | – |
| 8.0T (bore 14-25 mm) | – | 10-15 |