
Walk down the workholding aisle at any machine tool exhibition and you will see two kinds of machine vises side by side: the familiar hand-cranked precision vise, and the hydraulic vise with its pressure gauge and slim hose running back to a pump. They look similar, they hold parts the same way, yet the price gap is often three to five times. Whether a hydraulic vise is worth it depends on clamping force, repeatability, and batch size rather than on brand loyalty. This guide breaks down how each type works, where the real numbers land, and when the upgrade actually pays for itself on a CNC machining center.
The Quick Answer
A manual precision vise is the right choice for short runs, prototype work, and light-to-medium cuts where an operator tightens each part by hand. A hydraulic vise earns its keep in production machining: it delivers higher and fully repeatable clamping force with a quarter turn of a lever, which means less part movement, less scrap, and dramatically faster load-unload cycles across hundreds of parts. If you run the same job for a shift or more, hydraulics usually pay back within months; if every job is different, a good manual vise remains the more sensible tool.
How a Hydraulic Vise Actually Works
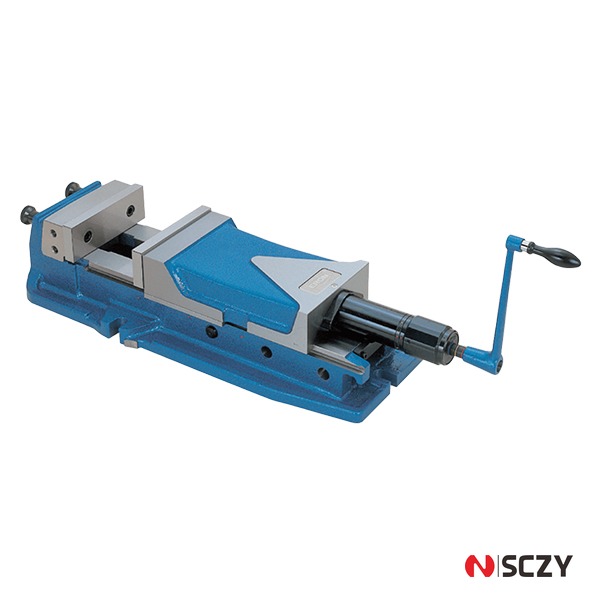
Inside the body of a hydraulic vise sits a compact hydraulic cylinder connected to the movable jaw. When the operator pulls the lever or turns the hand pump, pressurized oil pushes a piston that drives the jaw slide forward with a force far beyond what a thread screw can produce from the same handle effort. A relief valve in the circuit sets the maximum pressure, and therefore the maximum clamping force, which is the key to the whole design.
The Cylinder Does the Work, Not Your Wrist
With a screw vise, the operator generates force through a lead screw, and the actual force varies with how hard each person cranks the handle. With a hydraulic vise, the operator only positions the jaw against the part; the pressurized oil supply applies the final clamping force. Because that pressure is set once on the gauge, every part in the batch is squeezed with the same force. This is why shops moving from manual to hydraulic vises often report an immediate drop in thin-wall distortion and in “mystery” tolerance drift between the first part and the fortieth.
Reading the Pressure Gauge
Most hydraulic vises display clamping force as a function of hydraulic pressure. As a rule of thumb, doubling the gauge pressure roughly doubles the jaw force, and the relationship stays linear until the relief valve opens. The important habit is to write the set pressure into the setup sheet, the same way you would record tool offsets, so any operator reproduces the same clamp on the next shift.
Manual Vises: Where They Still Win
None of this makes the manual vise obsolete. For many shops it remains the workhorse, and for good reasons that have nothing to do with nostalgia.
Short Runs and Changing Work
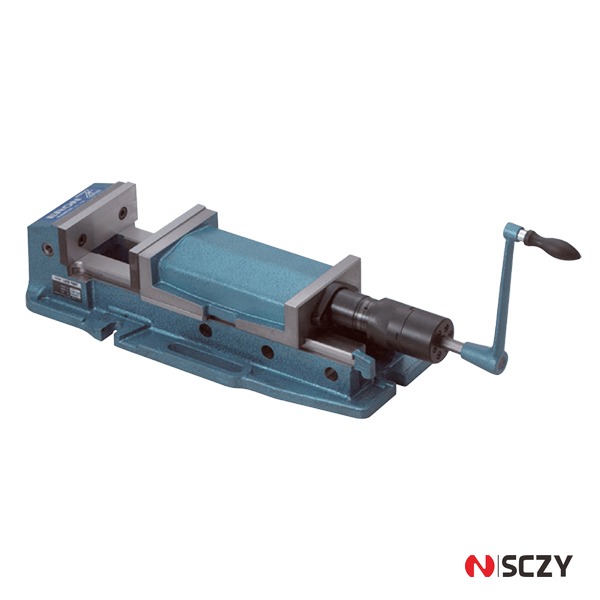
When the shop table changes jobs every hour, the hydraulic advantage in repeat clamping barely gets used. A quality manual precision vise sets up just as fast, needs no hose or pump on the table, and moves between machines without any plumbing. Job shops, mold repair benches, and prototype cells typically run dozens of one-off parts per day, and a hand-cranked vise handles all of them without a single extra accessory.
Cost, Simplicity and Maintenance
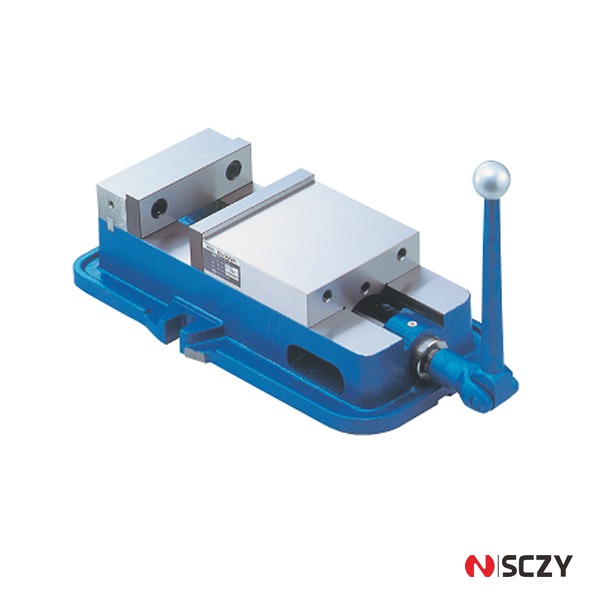
A precision manual vise costs a fraction of a hydraulic unit and its pump, contains no seals to age and no oil to leak, and can be rebuilt with basic hand tools. There is also a floor-space argument: hydraulic setups need a clear path for the hose and somewhere to mount the pump unit, which can be awkward on a small VMC table. For many shops the best first investment is simply a better manual vise with hard jaws that register accurately.
Clamping Force: The Real Numbers
Marketing sheets sometimes quote clamping force loosely, so it helps to think in kilonewtons and to separate typical values from peak ratings.
What a Hand-Cranked Screw Produces
A strong operator leaning on the handle of a 125 mm manual vise produces roughly 15 to 30 kN of jaw force, and a more careful operator tightening the same screw may produce half of that. The problem is not the maximum but the spread: the force depends on the person, the day, and how much torque they think the part needs. There is also a hard ceiling set by thread friction and by the risk of lifting the workpiece as the screw tightens.
What the Hydraulic Circuit Delivers
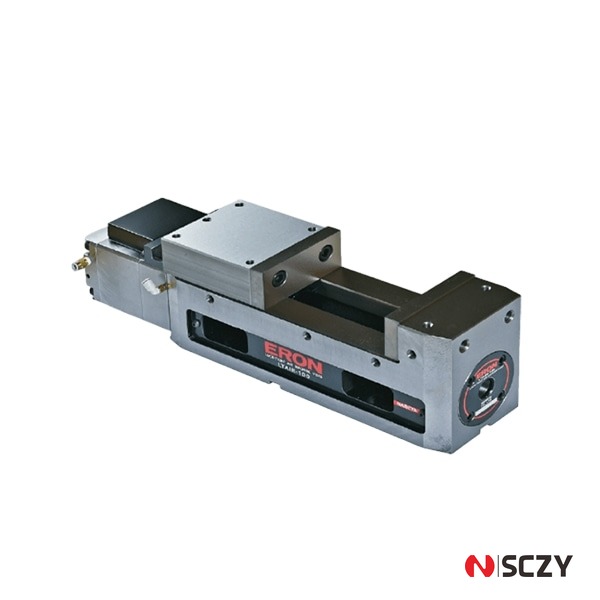
A hydraulic vise running at a typical 150 to 250 bar delivers 25 to 60 kN of clamping force on compact bodies, and larger models go further. More importantly, that force is identical on part one and part five hundred, because it comes from a regulated pressure rather than a human wrist. For heavy face milling, interrupted cuts, or roughing on hardened material, the extra force and the certainty behind it matter more than the headline number itself.
Repeatability and Part Quality
Clamping force is only half the story. In production, the question that decides scrap rates is whether part number 300 sits in exactly the same position as part number 1.
Jaw Lift and Part Movement
When a screw vise is tightened hard by hand, the movable jaw can lift slightly as the screw thread cams upward, tilting the part away from its seat. Skilled operators compensate by tapping the part down after tightening, but that step varies between people. Hydraulic jaws advance along a guided slide and clamp forward in one motion, so the part stays seated against the parallels. In practice this shows up as flatter first-operation surfaces and fewer surprises when the second operation references the first.
Why Repeatability Matters More in Production
On a one-off part, a careful operator can verify seating manually and move on. On a 400-piece batch running lights-out overnight, there is nobody to verify anything. Repeatability is what lets you trust the process when nobody is watching, and it is the single biggest quality reason shops specify hydraulic vises for unattended machining.
Side-by-Side: Manual vs Hydraulic vs Pneumatic
Pneumatic vises sit between the two, using shop air at around 6 bar with an internal area booster to reach useful force. Here is how the three types compare on the factors that matter in daily use.
| Factor | Manual precision vise | Hydraulic vise | Pneumatic vise |
|---|---|---|---|
| Clamping force | About 15-30 kN, operator-dependent | 25-60 kN+, pressure-regulated | About 10-25 kN, air-supply-dependent |
| Force repeatability | Poor to fair, varies by operator | Excellent, set on gauge | Good, set by regulator |
| Load-unload speed | Two or more crank turns per part | Quarter-turn lever per part | Fast lever or pedal, air actuated |
| Thin-wall safety | Risk of overtightening | Preset low pressure protects parts | Moderate, limited by air pressure |
| Power requirement | None | Hydraulic pump unit and hose | Clean, dry shop air at 6 bar |
| Typical use | Prototypes, short runs, toolroom | Production batches, heavy cuts | Mid-volume loading, fixture plates |
When the Upgrade Pays Off
The economics are straightforward once you count the minutes. If a manual vise costs 30 seconds of extra crank-and-check time per part compared with a quarter-turn hydraulic clamp, a 300-piece batch saves 150 minutes per run. Run that job monthly and the hydraulic premium disappears quickly, before you even count the scrap avoided through repeatable force.
Batch Size Is the Deciding Variable
As a practical threshold, shops running batches under roughly 20 pieces rarely recover the hydraulic investment, while shops running 100 or more of the same part usually do. The gray zone between depends on cycle time, part value, and how many vises you would need to convert. A useful exercise: pick your three highest-volume repeating jobs, multiply the per-part saving by annual quantity, and compare it against the price difference.
Hard Parts and Aggressive Cutting
The second trigger is cutting data. If your process calls for full-width face milling, interrupted cuts on forgings, or high-speed roughing in hardened steel, the higher regulated force of a hydraulic vise directly reduces the risk of part lift and chatter. Combined with the right tool holding, it is one of the cheapest ways to buy process margin on a machine that is already capable.
Pneumatic and Multi-Station Options Worth Knowing
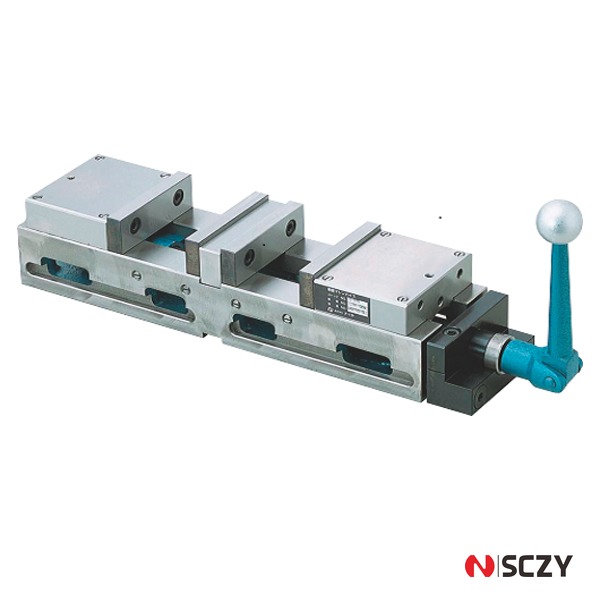
Before committing, check whether shop air infrastructure changes the comparison. A pneumatic vise clamps with a lever or pedal and releases instantly, which suits loading stations where operators handle parts every few seconds; its force ceiling is lower than hydraulics, so it fits aluminum, brass and mid-size steel parts rather than heavy roughing. For volume work, double-station vises clamp two parts in one body, letting the operator load one station while the machine cuts the other. We covered related layouts in our guide to pneumatic chucks for CNC machining, and jaw selection is treated separately in our vise jaws comparison.
Sizing and Installation Checklist
Whichever type you choose, a few checks prevent the most common regrets.
Jaw Opening and Part Envelope
Size the vise for the largest recurring part, not the largest part you might ever see. Check jaw opening with the soft jaws you actually plan to run, measure the clear height under the jaw plates, and confirm the part will not foul the screw or cylinder at full open. On hydraulic models, confirm the minimum part height too, since the jaw needs stroke travel to build pressure against short workpieces.
Mounting, Access and Safety
Plan the mounting before the vise arrives: manual vises need clean T-slots and access for the handle through its full sweep, hydraulic units need a hose route that cannot be pinched and a pump location away from chips, and pneumatic units need a regulator and filter reachable for daily checks. Clamp force always acts on whatever is under the part, so keep parallels and the vise bed clean, and never let setups rely on wedge effects from swarf.
Final Recommendation
Choose a manual precision vise when jobs change constantly, parts are small, and cutting forces are moderate. Choose a hydraulic vise when the same part repeats by the hundreds, when cuts are heavy, or when unattended machining demands force you can set and forget. In between, pneumatic and multi-station vises cover mid-volume loading at modest cost. The right vise is the one that matches your batch reality, and getting that match right improves accuracy more than any single cutting tool upgrade.
Not sure which clamping force or vise size fits your parts? Send us your workpiece drawings and batch quantities – the SCZY team will recommend the right hydraulic, pneumatic or manual vise configuration for your machines, with a practical quotation and lead time.



