
Every shop knows the usual rotation of tool holders: ER collets for versatility, Weldon side-lock holders for roughing, shrink-fit chucks for high-speed work. The hydraulic tool holder — sometimes sold as a hydraulic expansion chuck — sits quietly in the third drawer of the tool crib and quietly outperforms all three in the one job nobody budgeted for: cutting with calm. The difference is not marketing. It is a sealed oil chamber that behaves like a tuned damper, wrapped around a sleeve that clamps your tool in a perfectly concentric grip. This guide explains how the oil chamber works, what it actually buys you in runout, damping and thin-wall clamping, where its torque limits bite, and how to keep one alive for years instead of months.
How a Hydraulic Expansion Chuck Works
The Oil Chamber and the Clamping Sleeve
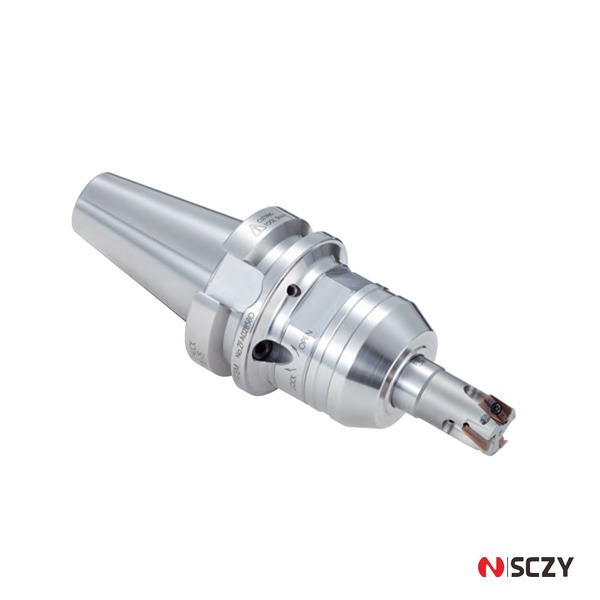
Inside the body of a hydraulic expansion chuck is a cylindrical cavity filled with a specially formulated oil. Inside that cavity sits a thin-walled steel clamping sleeve. When you tighten the clamping screws, internal pressure pushes the oil evenly in all directions, and the sleeve contracts uniformly around the tool shank. There are no slits, no jaws, no screw pressing directly on your cutter.
Because the pressure is hydrostatic, the sleeve cannot close unevenly the way a slitted ER collet can. The entire 360° surface of the bore presses against the shank with identical force. That is the root of almost every advantage — and every limitation — discussed below.
Why Oil Beats Springs for Holding a Tool
A collet grips through elastic deformation of slitted spring steel. If the shank is slightly undersize, slightly dirty, or slightly off-round, the contact pattern becomes a lottery: a few contact bands carry the load, the rest of the bore is air. The hydraulic sleeve flexes a few microns instead, conforming to the actual shank. Small diameter errors, minor flute marks and light contamination are absorbed rather than converted into runout or slip.
Damping: The Real Reason Surface Finish Improves
What Oil Damping Does to Chatter
The single most under-appreciated property of a hydraulic tool holder is damping. Metal transmits vibration almost without loss; oil converts vibration into heat. A cutting tool held in a hydraulic chuck is, in effect, mounted on a tiny shock absorber. When the cutter tooth hits a hard spot or an interrupted cut, the resulting shock is dissipated in the oil film instead of ringing through the shank and into your spindle.
On the shop floor this shows up as chatter marks fading from the workpiece, a quieter cut, and flank wear instead of chipped edges. Toolmakers commonly report 30–60% longer tool life on thin-wall and finishing work simply by moving the same cutter from an ER collet into a hydraulic expansion chuck. Your numbers will vary, but the direction does not.
Where Damping Pays for Itself
Three situations repay the price of a hydraulic holder fastest:
- Thin-wall parts — ring sections, aerospace brackets, thin flanges. A damped cut transmits less energy into the part, so the wall does not act like a tuning fork.
- Small-diameter tools — everything under 8 mm. A tiny deflection that would break a 3 mm carbide end mill in a stiff holder is absorbed in oil.
- Deep-cavity mold cores — long projections amplify any vibration. Damping at the holder is the cheapest place to remove it.
Runout: Why 3 Microns TIR Is Repeatable, Not Lucky
Quality hydraulic chucks hold a TIR (total indicated runout) of ≤3 µm at 3× the shank diameter — and, critically, they repeat it. Runout in a collet chuck depends on how the slits align, how clean the bore was, and how the nut was torqued. In a hydraulic chuck the sleeve is centered by the oil film itself; there is no mechanical decision to get wrong. Tighten the screws to spec and the grip is geometrically identical every time.
For shops running lights-out or holding ±5 µm tolerances, that repeatability is the reason hydraulic holders earn their keep even where torque is not an issue. If you are comparing holders for a job that mixes finishing and drilling, remember that runout affects drill life more than any other tool type — see our ER collet runout guide for the measurement details.
Hydraulic vs Collet vs Shrink-Fit: The Honest Comparison
The three precision holders overlap, but each dominates a different slice of the work. Here is the comparison in plain numbers:
| Property | Hydraulic Expansion Chuck | ER Collet Chuck | Shrink-Fit Holder |
|---|---|---|---|
| TIR at 3×D | ≤3 µm, highly repeatable | ≤5–10 µm, depends on setup | ≤3 µm, repeatable |
| Damping | Excellent (oil chamber) | Low | Low–moderate (stiff body) |
| Torque transmission | Moderate — the weak point | Good | Excellent |
| Tool change speed | Fast (hex screws, no induction heater) | Fast | Slow (heating cycle per change) |
| Suitability for small dia. | Excellent, down to Ø2 mm and below | Good, but slit alignment matters | Excellent |
| Thin-wall workpieces | Best (damping protects the part) | Poor | Fair |
| Maintenance | Oil refill, seal checks | Collet cleaning, nut torque | Coil and body inspection |
| Typical cost | High | Low | High + heater investment |
One honest note: the comparison above assumes quality holders on both sides. A worn hydraulic chuck with tired seals can be worse than a fresh ER system — maintenance decides, as always. For the full three-way argument including prices and workholding context, see our dedicated comparison of collet, hydraulic and shrink-fit holders.
Torque Limits: Where Hydraulics Lose, and What to Do Instead
The same thin sleeve that gives you damping and runout gives you the hydraulic chuck’s one real weakness: torque capacity. A side-lock or power milling chuck transmits torque through a screw or an interlocking key; a hydraulic sleeve transmits it through friction on a smooth bore. Big carbide insert cutters, high-feed mills and heavy roughing will push past that friction and the cutter will creep or pull out.
So draw the line deliberately:
- Use hydraulic for finishing end mills, drills up to ~13 mm, reamers, chamfer tools and ball-nose work in mould steels and stainless.
- Do not use hydraulic for heavy roughing, high-feed milling or any cutter with a flat Weldon shank that was designed for a set screw.
- Between the two, consider a power milling chuck for roughing and keep hydraulics for the passes that decide the finish.
A practical shop pattern: rough in a side-lock or power chuck, then swap the same job into a hydraulic expansion chuck for the semi-finish and finish. The two holder types are complementary, not competing.
Thin-Wall and Micro-Tool Applications
Two application families deserve special mention because they are where hydraulic holders are genuinely irreplaceable.
Thin-wall machining. When the workpiece is more flexible than the toolholder, every joule of vibration you remove from the holder shows up as improvement on the part. Aerospace ring segments, thin flanges and medical implant blanks are the classic cases: same machine, same cutter, same program — only the holder changed, and the reject rate fell.
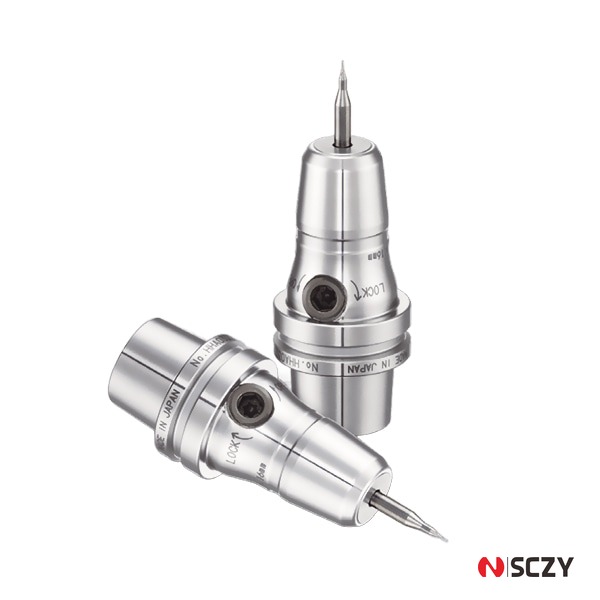
Micro-diameter tools. Below about 4 mm, carbide becomes fragile and forgiving margins vanish. The hydraulic sleeve grips without point loads, so there is no local stress raiser at the shank, and the damping saves cutters from the shock of entry. This is also where the slim-head designs shine: heads narrow enough to reach into pockets between ribs, as on the slender hydraulic holders shown below.
Setup and Care: Refilling, Seals and Temperature
The Screw-Tightening Procedure That Matters
Hydraulic chucks are torque-sensitive in a good way. Tighten the clamping screws progressively in a star pattern (or sequentially, per the manufacturer’s diagram) to the printed torque — usually 8–13 Nm for common sizes. Overtightening does not increase grip; it overstresses the sleeve and can crack it. Undertightening leaves the oil pressure incomplete. A small click-type torque driver pays for itself with the first sleeve you do not have to replace.
Oil Refill and Seal Kits
The oil chamber is sealed, but refill ports exist because oil slowly weeps past sleeve seals over thousands of clamping cycles. Symptoms of low oil pressure are subtle: slightly higher runout, slightly more chatter, a grip that feels soft. Most manufacturers sell refill kits with a metered syringe and the correct oil viscosity — do not improvise with hydraulic jack oil; viscosity and anti-foam additives differ. Check refill intervals in the manual, typically every 2–3 years in normal service, sooner in hot shops running 2+ shifts.
Temperature and Storage Rules
Standard hydraulic oil starts to thin around 60–80 °C. That is well beyond anything cutting heat will reach inside the holder body, but it rules out mounting hydraulic holders near induction shrink-fit stations or steam lines. For storage, treat them like any precision holder: clean taper, protective cap, dry cabinet. Our tool holder maintenance routine covers the full procedure.
Buying Checklist: Five Specs to Check Before You Order
Before you add hydraulic expansion chucks to the tool crib, verify these five things with the supplier:
- Clamping diameter range — the sleeve is a fixed bore, not a range. Plan one holder per cutter diameter (or use stepped sleeves where offered).
- TIR spec and measurement distance — insist on ≤3 µm at 3×D measured at the shank, not “runout” quoted at the nose.
- Balancing grade — for spindles above 12,000 rpm, ask for G2.5 balanced bodies; see our G2.5 vs G6.3 balancing guide for the reasoning.
- Projection and head diameter — slim heads trade some rigidity for access; match the head to your deepest pocket, not to the catalogue photo.
- Interface match — BT, BBT (dual contact), CAT and HSK bodies change stiffness and coolant options more than the hydraulic system itself does.
The Bottom Line
A hydraulic tool holder will not out-torque a power milling chuck and does not try. What the hydraulic expansion chuck offers instead is a combination no other holder matches: micron-level repeatable runout, real vibration damping, a gentle and uniform grip on small shanks, and a cutting sound that stays calm when the workpiece is thin, hard or deep. Buy a few in your most-used finishing diameters, follow the torque procedure, refill the oil on schedule, and let them own the passes where surface finish and tool life are actually decided.
Need help matching hydraulic holders to your spindles and cutters — BT40, BBT40 or HSK? Contact the SCZY team for a selection review, sample holders and a quote for your specific jobs.



